High-Performance Industrial Pallet Racking Systems
Engineered to strictly adhere to international quality standards including CE (EN 1090-1 / EN 15512), FEM 10.2.02, and RMI MH16.1 specifications. Explore our core manufacturing portfolio designed for high-density warehouse storage.
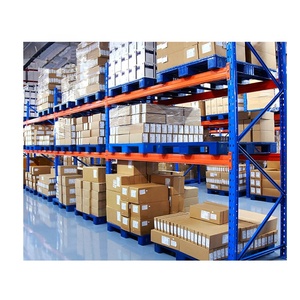
Heavy Duty Single Deep Industrial Selective Pallet Racks
Engineered with high-yield cold-rolled steel profiles for 100% direct SKU accessibility and maximum load stability up to 4500kg per beam level.
Technical Specifications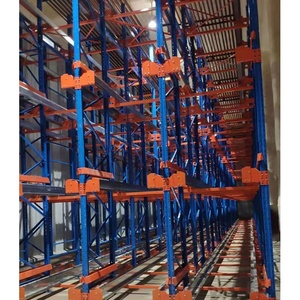
Industrial Radio Shuttle & Stacking Pallet Rack Systems
Semi-automated high-density storage solution integrating semi-autonomous shuttles to dramatically increase volumetric space utilization in cold chain storage.
Technical Specifications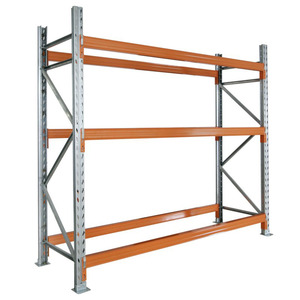
Full Automatic Q235B Boltless High-Bay Pallet Racking
Precision-manufactured structural framing designed for AS/RS integration, certified under strict European CE tolerances for automated stacker crane operations.
Technical Specifications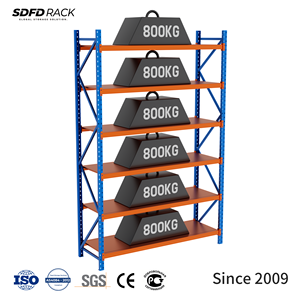
800kg–3000kg Heavy Duty Adjustable Selective Racks
Flexible multi-layer warehouse racking featuring 75mm/50mm pitch adjustments, robotic-welded beam connectors, and safety locking pins.
Technical Specifications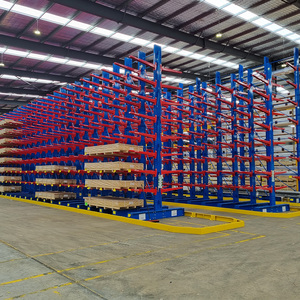
Heavy Duty Structural Steel Cantilever & Cold Room Racks
Specialized structural rack designs engineered for long, bulky loads and harsh low-temperature environments down to -30°C without structural embrittlement.
Technical Specifications
Adjustable Steel Structural Industrial Storage Systems
Heavy-duty roll-formed upright frames combined with step beams or box beams, finished with electrostatic powder coating for superior scratch and chemical resistance.
Technical Specifications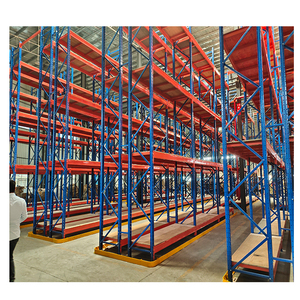
High-Density Industrial Selective Beam Racking Systems
Optimum strength-to-weight ratio utilizing premium Q355B cold-formed structural profiles, engineered to meet rigorous seismic design criteria.
Technical Specifications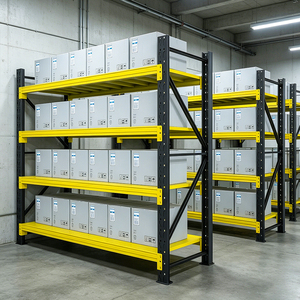
Modular Tire Stacking & Small Parts Warehouse Racks
Versatile modular storage solutions tailored for automotive tire distribution centers, manufacturing parts rooms, and multi-tier picking platforms.
Technical SpecificationsEngineering Leadership & Factory Manufacturing Strengths
As a global tier-one manufacturer of industrial warehouse storage solutions, our enterprise combines near 70-year structural manufacturing heritage with state-of-the-art automated production technology. Operating out of expansive, ISO 9001 and ISO 14001 certified manufacturing facilities, we specialize in delivering CE certified warehouse pallet racking systems engineered for demanding commercial and industrial application environments.
Rigorous Structural Engineering
Every upright frame, beam profile, and bracing member undergoes rigorous Finite Element Analysis (FEA) modeling and physical destructive load testing. Designed in strict compliance with EN 15512, RMI 2012, and FEM 10.2.02 design codes.
Automated Manufacturing Lines
Multi-million dollar investments in automated continuous roll-forming lines, robotic welding cells, and multi-stage automated powder coating lines guarantee dimensionally uniform components with zero structural deflection variance.
Full CE Factory Compliance
Holding Factory Production Control (FPC) certification under EN 1090-1 Execution Class 2 (EXC2). Every batch of raw structural steel (Q235B / Q355B) is supplied with complete Mill Test Certificates (EN 10204 3.1) guaranteeing chemical and mechanical properties.
Technological & Structural Development Trends in Industrial Storage
The industrial warehousing landscape is experiencing a paradigm shift driven by rising urban real estate costs, supply chain velocity requirements, and stricter workplace safety regulations. Modern warehouse infrastructure is moving rapidly from passive storage frameworks to dynamic, load-optimized structural ecosystems.
1. Transition to High-Yield Micro-Allayed Steel Profiles
Traditional pallet rack manufacturing relied heavily on standard structural carbon steel (Q235B). Modern CE-certified manufacturing facilities have transitioned to micro-alloyed, high-strength steel grades such as S355MC and Q355B. These cold-formed profiles provide a significantly higher yield strength ($f_y \ge 355 \text{ MPa}$ compared to $235 \text{ MPa}$), allowing manufacturers to reduce dead load weight by 12% to 18% while simultaneously elevating total permissible rack column loading capacity.
2. Integration of Semi-Automated and Autonomous AS/RS Interfaces
As labor costs escalate globally, racking systems are increasingly designed to interface directly with Radio Shuttles, Autonomous Mobile Robots (AMRs), and Automated Storage and Retrieval Systems (AS/RS). This requires structural manufacturing tolerances far tighter than standard commercial racking:
| Racking Technology Category | Volumetric Density Efficiency | Structural Manufacturing Tolerance | Primary Industrial Use Case |
|---|---|---|---|
| Selective Pallet Racking | 40% – 50% Space Utilization | Standard ($\pm 3.0 \text{ mm}$) | High SKU count, direct 100% pallet access required. |
| Radio Shuttle High-Density Rack | 70% – 85% Space Utilization | Precision ($\pm 1.5 \text{ mm}$) | Cold storage, food & beverage, high-volume batch goods. |
| AS/RS High-Bay Structural Rack | 85% – 95% Space Utilization | Ultra-Precision ($\pm 0.8 \text{ mm}$) | 24/7 Fully automated logistics centers, high-vertical bays. |
3. Advanced Anti-Corrosion Surface Finishing for Harsh Environments
Industrial facilities in humid tropical zones, coastal logistics hubs, and cold storage operations demand advanced surface protection. State-of-the-art factories now employ a multi-stage pretreatment process involving zinc-phosphate washing, followed by electrostatic application of thermosetting epoxy-polyester powder coats (60–90 microns thick). For extreme environments, hot-dip galvanizing (HDG) conforming to ISO 1461 ensures multi-decade structural integrity against corrosion.
Future Procurement Trends for Pallet Racking Systems
Global logistics procurement officers and warehouse engineering consultants are re-evaluating sourcing models to balance capital expenditure (CAPEX), total operational risk, and long-term modular flexibility.
Direct Factory Sourcing & OEM/ODM Engineering
Intermediary distributors are increasingly bypassed in favor of direct engagement with CE-certified rack factories. Direct factory collaboration grants access to custom column punching, specialized beam profiles, and tailored CAD/BIM modeling directly from manufacturer engineering departments.
Lifecycle Carbon Accounting & CBAM Readiness
With the implementation of the European Union’s Carbon Border Adjustment Mechanism (CBAM), procurement criteria now include environmental product declarations (EPDs). Sourcing from factories utilizing energy-efficient electric arc furnaces (EAF) and recyclable steel significantly lowers Scope 3 embedded carbon emissions.
Modular Reconfigurability & Standardization
Modern supply chains demand modular adaptability. Sourcing standardized teardrop or 75mm euro-pitch beam connectors ensures that storage layouts can be expanded, elevated, or converted from selective racking to drive-in or carton-flow systems without replacing base upright frames.
Procurement FAQ: Engineering & Compliance Guide
Critical technical answers to address structural integrity, certification compliance, seismic engineering, and global export verification when procuring heavy-duty pallet racking systems.
What does CE certification specifically guarantee in warehouse pallet racking?
CE certification for industrial pallet racking indicates strict compliance with European Regulation (EU) No 305/2011 (Construction Products Regulation or CPR) and standard EN 1090-1 / EN 15512. It verifies that the factory operates a certified Factory Production Control (FPC) system, raw materials are fully traceable with EN 10204 3.1 mill test certificates, welders are qualified under ISO 9606-1, and structural load capacities are validated by rigorous finite element calculation models.
How is the maximum load capacity per beam level calculated safely?
Beam load capacity is determined based on both yield strength criteria and deflection limits. Under EN 15512 and RMI specifications, the maximum allowable vertical deflection of a beam under full design load must not exceed $L/200$ (where $L$ is the clear span length between upright columns). Furthermore, a safety factor of at least 1.65 against material yield is built into structural capacity calculations.
What structural parameters are required to design a seismic-resistant racking system?
To design for seismic zones (e.g., compliant with Eurocode 8 or US FEM 10.2.08 criteria), engineers require local ground acceleration values ($a_g$), soil type classification, building duct characteristics, and concrete slab specifications. Seismic-resistant racking utilizes enlarged base plates, heavy-duty wedge anchor bolts, reinforced frame bracing, and custom column footings to absorb lateral shear and overturn moments during dynamic earthquake events.
What is the difference between Q235B and Q355B structural steel in rack manufacturing?
Q235B is a standard carbon steel profile with a minimum yield strength of $235 \text{ MPa}$, widely used for standard light-to-medium duty racking application. Q355B is a high-strength, low-alloy structural steel offering a minimum yield strength of $355 \text{ MPa}$ (~51% higher strength). Utilizing Q355B allows for higher upright column loading capacity, slimmer structural profiles, and enhanced resistance to localized forklift impact stresses.
How do you ensure proper anti-corrosion protection for cold room and freezer storage applications?
For sub-zero cold storage facilities down to -30°C, steel embrittlement and moisture condensation are critical threats. We recommend either hot-dip galvanized finishes (zinc coating thickness $\ge 65 \, \mu\text{m}$) or high-grade electrostatic powder coating with a dedicated zinc-rich primer base. Additionally, structural steel grades with tested Charpy V-notch impact toughness at low temperatures are selected to prevent brittle fractures.
What critical documentation should be provided upon order completion?
A certified factory supply package must include: (1) Certificate of CE Conformity and Factory Production Control (FPC) documentation, (2) Raw Material Mill Test Certificates (EN 10204 3.1), (3) Detailed Structural Layout CAD Drawings with stamped loading charts, (4) Installation & Maintenance Guidelines conforming to EN 15635, and (5) Material Safety Data Sheets (MSDS) for surface paint treatments.
Need Custom CE Certified Pallet Racking Engineering?
Consult directly with our structural engineering team for warehouse layout planning, seismic calculation verification, factory-direct wholesale quotes, and OEM manufacturing requests.