Pallet Flow & Reserve Replenishment
Full pallet loads are fed via gravity flow lanes directly behind order picking faces, ensuring continuous automatic FIFO replenishment for high-turnover SKUs without cross-aisle forklift traffic.
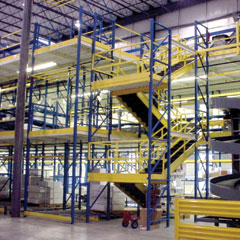
Multi-Level Work Platforms & Integrated High-Density Order Fulfillment Solutions
Pick Modules designed by CR Industrial Racks & Storage Co. are custom-engineered multi-level storage and work platform structures designed to streamline complex distribution workflows. By utilizing structural or heavy-duty roll-formed pallet racking as the core skeletal frame, our pick modules support miles of integrated conveyor routes, carton flow lanes, pallet flow systems, and push-back storage cells in a single consolidated footprint.
Engineered for global e-commerce fulfillment centers, mega third-party logistics (3PL) facilities, and international distribution hubs, these systems consolidate full pallet staging, split-case picking, piece replenishment, and automated sortation across multi-tier elevated work platforms. Capable of handling hundreds of thousands of picks per day, CR Industrial Racks & Storage Co. pick modules deliver exceptional throughput efficiency while dramatically reducing pick travel times and order error rates.
Every pick module engineered by CR Industrial Racks & Storage Co. combines multiple high-density storage techniques into an ergonomic, multi-level fulfillment matrix.
Full pallet loads are fed via gravity flow lanes directly behind order picking faces, ensuring continuous automatic FIFO replenishment for high-turnover SKUs without cross-aisle forklift traffic.
Integrated gravity carton flow tracks present split cases and individual items directly at the operator's waist-high picking face, dramatically accelerating piece-picking speeds.
Heavy-duty rack beams support central power or gravity conveyor lines through each module walkway level, instantly transporting picked cartons directly to packing and shipping zones.
Engineered structural floor decking, grating, safety handrails, and integrated stair towers provide comfortable, code-compliant access for personnel across multiple elevated work tiers.
Developing multi-level pick modules requires rigorous structural calculations. Upright columns, heavy-duty beam connections, base plates, and overhead bracing must resist dynamic conveyor forces, live human deck loads, and seismic horizontal acceleration forces.
CR Industrial Racks & Storage Co. designs every system strictly to current RMI (Rack Manufacturers Institute) standards and ANSI MH16.1 specifications. Our international engineering team provides complete stamped load capacity calculations, seismic zone evaluations, slab embedment stress analyses, and precise layout drawings for seamless overseas project commissioning.
Overview of structural tolerances, deck configurations, and integrated components engineered by CR Industrial Racks & Storage Co.
| System Parameter | Technical Specification / Capability |
|---|---|
| Platform Tiers | 1 to 4 Elevated Work Levels (Custom Vertical Heights up to 15+ Meters) |
| Structural Component Types | Heavy-Duty Roll-Formed Steel or Structural Channel Steel (Hot-Rolled) |
| System Integration Types | Pallet Flow, Carton Flow, Push-Back, Selective Pallet Storage, Power/Gravity Conveyors |
| Mezzanine Decking Options | Bar Grating, ResinDek Floor Panels, Diamond Steel Plate, Heavy-Duty Plywood Decking |
| EHS & Safety Compliance | Integrated Stair Towers, Safety Cages, Kickplates, Mesh Fall Protection, Fire Baffle Integration |
| Corrosion Protection & Finish | Automated Uniform Powder Coat Paint Line (Custom Industrial Color Schemes Available) |
| Design & Quality Standards | RMI Specifications, ANSI MH16.1, ISO 9001 Manufacturing Quality Standards |
Our dedicated engineering specialists provide CAD layouts, load capacity calculations, and custom structural proposals tailored to your facility's exact throughput goals.
Inquire NowA pick module is an engineered multi-level work platform that uses heavy-duty pallet rack frame structures to support product flow systems (carton flow, pallet flow, push back) integrated with conveyor transport lines to optimize piece and case order picking across vertical facility space.
By taking advantage of vertical warehouse height, multi-level pick modules reduce operator travel time, consolidate high SKU counts into organized picking faces, separate replenishment from order picking, and facilitate continuous conveyor-based order consolidation.
Yes. All pick modules manufactured by CR Industrial Racks & Storage Co. are engineered strictly in accordance with RMI (Rack Manufacturers Institute) and ANSI MH16.1 specifications, including custom seismic design calculations for global installations.
To design an optimal system, our engineering team requires building clear heights, floor slab concrete depth and strength ratings, pallet load weights/dimensions, daily order velocity targets, SKU counts, and conveyor layout specifications.