Featured CE Certified Racking Systems
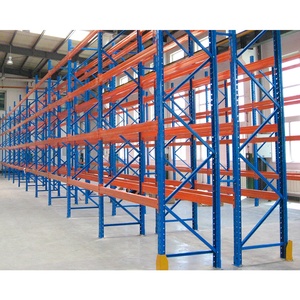
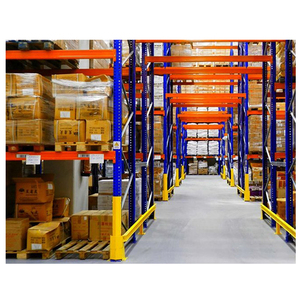
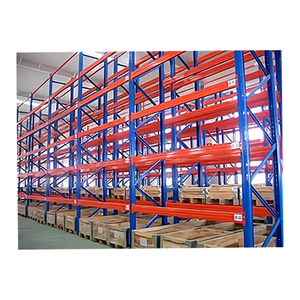
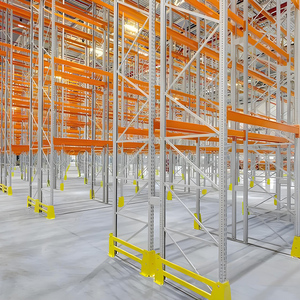
Explore our top-tier heavy-duty storage equipment, engineered for high structural stability, maximum volumetric efficiency, and strict European CE safety compliance.
Engineering Heritage & Enterprise Manufacturing Advantages
Selecting an industrial storage rack manufacturer is a critical decision impacting operational safety, structural resilience, and long-term capital efficiency. As a leading manufacturer and global wholesaler of CE Certified Industrial Storage Racks, our corporate foundation is built on nearly 70 years of continuous structural steel innovation and engineering perfection.
Modern supply chain logistics demand more than just static steel beams; they require rigorously tested, finite-element-analyzed racking structures capable of enduring dynamic forklift impacts, seismic accelerations, and continuous micro-vibrations. Our manufacturing facilities utilize advanced automated cold-roll forming lines, robotic welding stations, and multi-million-dollar electrostatic powder coating systems.
CE & EN 15512 Certification
Every beam, upright frame, and connector pin is engineered and manufactured to strict European EN 15512 structural standards, ensuring full safety compliance across EU and global free trade zones.
Advanced Powder Coating
Automated multi-stage wash and electrostatic thermosetting powder coat lines deliver uniform, high-mil corrosion protection designed for high-humidity and tropical warehouse environments.
Seismic Structural Design
In-house structural engineering teams conduct Finite Element Analysis (FEA) to verify base plate thickness, anchor bolt embedment depth, and dynamic sway resistance under high-risk seismic codes.
Industrial Storage Racks Architecture & System Selection Guide
Optimizing warehouse cubic space while maintaining seamless inventory rotation requires aligning the physical characteristics of your goods with the ideal structural racking topology. Below is an engineering overview of the primary industrial storage rack architectures manufactured for wholesalers and enterprise end-users.
1. Selective Pallet Racking Systems (Structural & Roll-Formed)
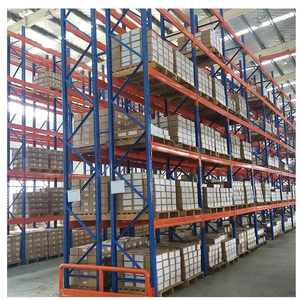
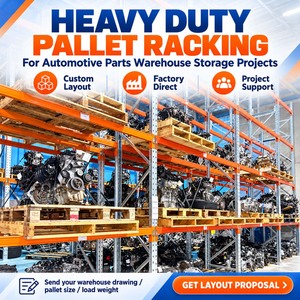
Selective pallet rack remains the workhorse of global logistics due to its 100% direct pallet accessibility. Manufactured from either high-yield Q235B roll-formed steel or Q355B hot-rolled structural steel channels, selective systems allow independent adjustments of beam elevations on 50mm or 75mm pitches. Ideal for operations with high SKU counts and continuous SKU movement.
2. High-Density Drive-In & Drive-Thru Racks
For operations handling bulk goods with low SKU variance—such as cold chain agricultural exports, beverage bottling plants, and raw material archives—Drive-In racking eliminates traditional forklift aisles. Forklifts enter the racking lanes directly to load and retrieve pallets stored on continuous heavy-duty support rails. This configuration increases cube storage density by up to 75% compared to selective rack layouts.
3. Specialized Roll-Out & Crank-Out Cantilever Racks
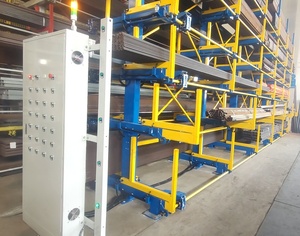
Storing long, bulky, or irregular materials like aluminum extrusions, steel tubing, timber, and heavy molds presents severe handling hazards. Our CE Certified Roll-Out Cantilever Racks incorporate smooth mechanical crank extension mechanisms that extend the storage arms completely outside the rack structure. This allows overhead gantry cranes or hoists to perform vertical direct lifts, eliminating manual forklift maneuvering risks and drastically reducing loading cycles.
4. Dynamic Gravity Flow & Push-Back Racks
Utilizing tilted roller beds or nested cart channels, dynamic racking uses gravity to drive inventory forward. Pallet Flow Racks enforce strict First-In, First-Out (FIFO) stock rotation—crucial for perishable pharmaceuticals and food products. Push-Back Racks operate on a Last-In, First-Out (LIFO) framework where incoming pallets push existing carts back, maximizing density up to 6 pallets deep per lane without forcing forklifts into the structure.
Future Global Procurement Trends in Industrial Storage Racking
The global warehousing and logistics landscape is undergoing a massive transformation driven by land cost escalation, rapid e-commerce proliferation, and strict environmental regulations. B2B procurement managers and wholesale buyers must evaluate emerging technical vectors when sourcing industrial racking equipment:
A. Automation-Ready & ASRS Structural Compatibility
Traditional manually operated racking is rapidly giving way to Automated Storage and Retrieval Systems (ASRS), Autonomous Mobile Robots (AMRs), and Pallet Shuttles. Modern procurement strategies require purchasing structural racks fabricated to ultra-tight millimetric tolerances. Deflection tolerances must be calculated under strict L/240 or L/300 dynamic beam flexure parameters to ensure automated shuttle wheels and optical guidance sensors operate without jamming.
B. Low-Carbon Steel & Eco-Friendly Powder Formulations
Environmental, Social, and Governance (ESG) mandates are now mandatory criteria in global tenders. Industrial racking buyers are increasingly favoring manufacturers utilizing zero-VOC electrostatic powder coatings, closed-loop water treatment facilities, and scrap-reducing automated cold-roll lines. Sourcing high-strength micro-alloyed steel enables reduced metal gauge thickness while preserving structural load capacity, resulting in lower shipping weight and a reduced carbon footprint.
C. Modular Safety Customization & Impact Resilience
Occupational safety regulators (OSHA, EU Machinery Directive) have placed warehouse rack integrity under intense scrutiny. Future racking procurement heavily emphasizes integrated passive and active safety systems: structural column wraparound protectors, heavy-duty end-of-aisle guardrails, drop-in wire decking with reinforced channels, and quick-replacement bolt-on frame repair kits that allow structural upright restoration without full system dismantling.
Next-Generation Racking Innovations & R&D Strategy
Our research and development division is actively pioneering several structural breakthroughs that re-define warehouse safety and storage density:
IoT Load-Cell Integration
Embedding smart piezoelectric stress sensors directly into primary beam connections to provide real-time weight telemetry, detecting overloading and structural fatigue before dynamic failure occurs.
High-Tensile Micro-Alloy Profiles
Transitioning to ultra-high-yield Q355B and Q460 cold-rolled structural alloys to minimize steel deadweight while enhancing total frame capacity by up to 28% under equal profile dimensions.
Nan-Coated Salt-Spray Coatings
Formulating advanced zinc-rich primer and polyurethane topcoat treatments certified to withstand 1,000+ hours of continuous salt-spray testing—ideal for coastal logistics ports and chemical plants.
Procurement FAQ: Technical & Wholesaler Inquiries
Below are detailed responses to the most critical technical, compliance, and logistics questions asked by enterprise purchasers, logistics engineers, and wholesale partners.
CE Certification for industrial storage racking is governed by European Standard EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design) along with EN 1090 for structural steel execution. Achieving CE status requires comprehensive destructive compression testing on upright frames, beam end-connector stub testing, shear testing of safety locks, and full bending moment analysis. As certified manufacturers, our production lines undergo third-party Factory Production Control (FPC) audits to ensure material traceability, weld quality, and dimensional consistency.
Seismic design requires calculating lateral dynamic shear forces according to localized seismic zone codes (such as RMI/ANSI MH16.1, US IBC, or local structural standards). Our engineering team performs 3D Finite Element Analysis (FEA) to simulate earthquake ground acceleration. Seismic-grade racking typically incorporates oversized heavy-duty base plates, thicker heavy-gauge anchor bolts with high embedment depths, heavy diagonal bracing patterns, and high-ductility steel connectors designed to absorb vibrational kinetic energy without brittle shear failure.
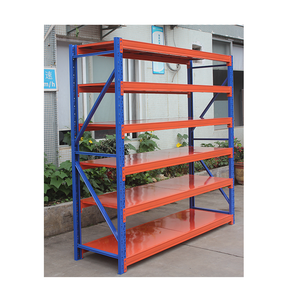
Roll-Formed Racking is manufactured by cold-forming sheet coil steel into teardrop or slotted channel profiles. It is highly cost-effective, versatile, and allows fast tool-less beam adjustment—making it ideal for general retail and warehousing. Structural Steel Racking is fabricated from hot-rolled C-channel structural steel assembled with heavy-duty structural bolts. Structural rack offers vastly superior impact resistance, higher weight capacities, and exceptional durability in harsh environments like freezer storage facilities and high-traffic manufacturing plants where forklift collisions are frequent.
To provide an accurate, load-rated structural racking proposal, our engineering team requires: (1) Pallet dimensions (Width x Depth x Height including load); (2) Maximum gross pallet weight; (3) Warehouse clear height underneath roof joists or sprinklers; (4) Floor slab thickness, concrete compressive strength (PSI/MPa), and rebar layout; (5) Forklift specifications including maximum lift height and minimum aisle turning radius; and (6) Environmental parameters such as operating temperature (cold store vs. ambient) and seismic requirements.
For high-humidity tropical sites, coastal port warehouses exposed to airborne salt, or wash-down food processing units, Hot-Dip Galvanizing (HDG) or heavy-duty outdoor-grade powder coating is essential. Hot-Dip Galvanizing submerges the steel components into molten zinc, forming a metallurgical alloy bond that provides sacrificial cathodic protection against rust—even if scratched. Alternatively, our automated multi-stage pre-treatment wash and epoxy-polyester powder coat lines provide a non-porous, corrosion-resistant surface ideal for freezer rooms down to -30°C.
Standard production lead time for full container loads (20GP / 40HQ) is typically 3 to 4 weeks from technical CAD drawing approval. As a dedicated OEM/ODM manufacturer, we supply wholesale distributors with custom color powder matching, private labeling, custom punch patterns, and tailored retail packaging. All components are densely bundled, corner-protected with heavy corrugated board, steel-strapped, and plastic-wrapped to prevent shift damage during ocean transit.
Partner with a Certified Heavy-Duty Racking Manufacturer
Ready to engineer your warehouse layout, request OEM wholesale pricing, or verify technical structural specifications? Connect with our senior storage engineering team today.
Inquire Now